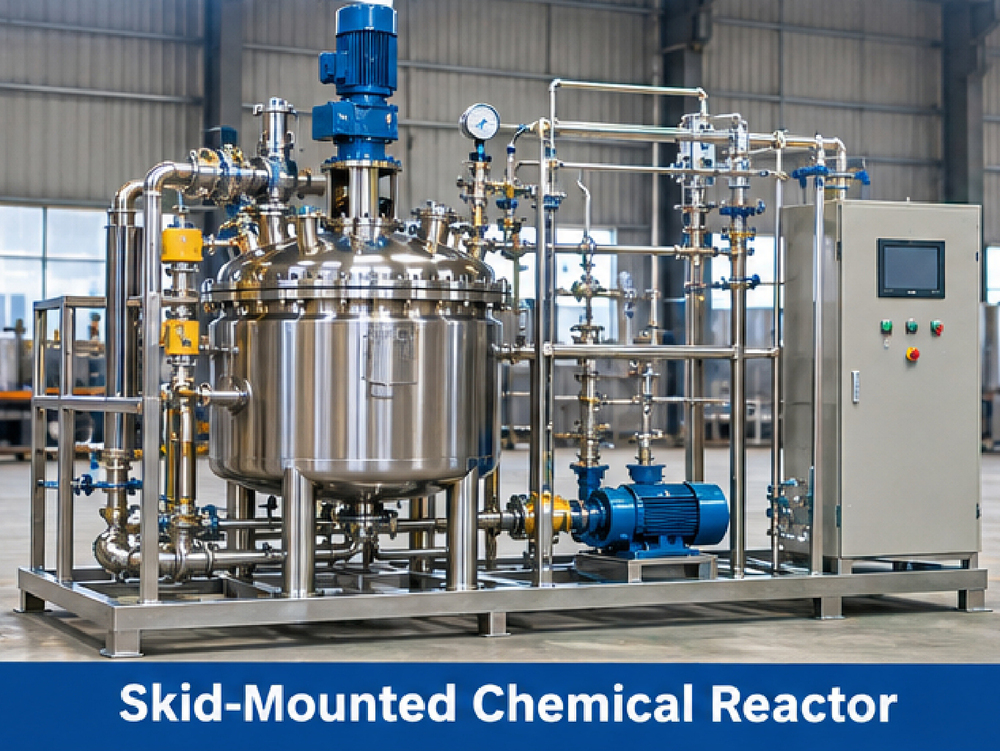
About Skid-Mounted Chemical Reactor
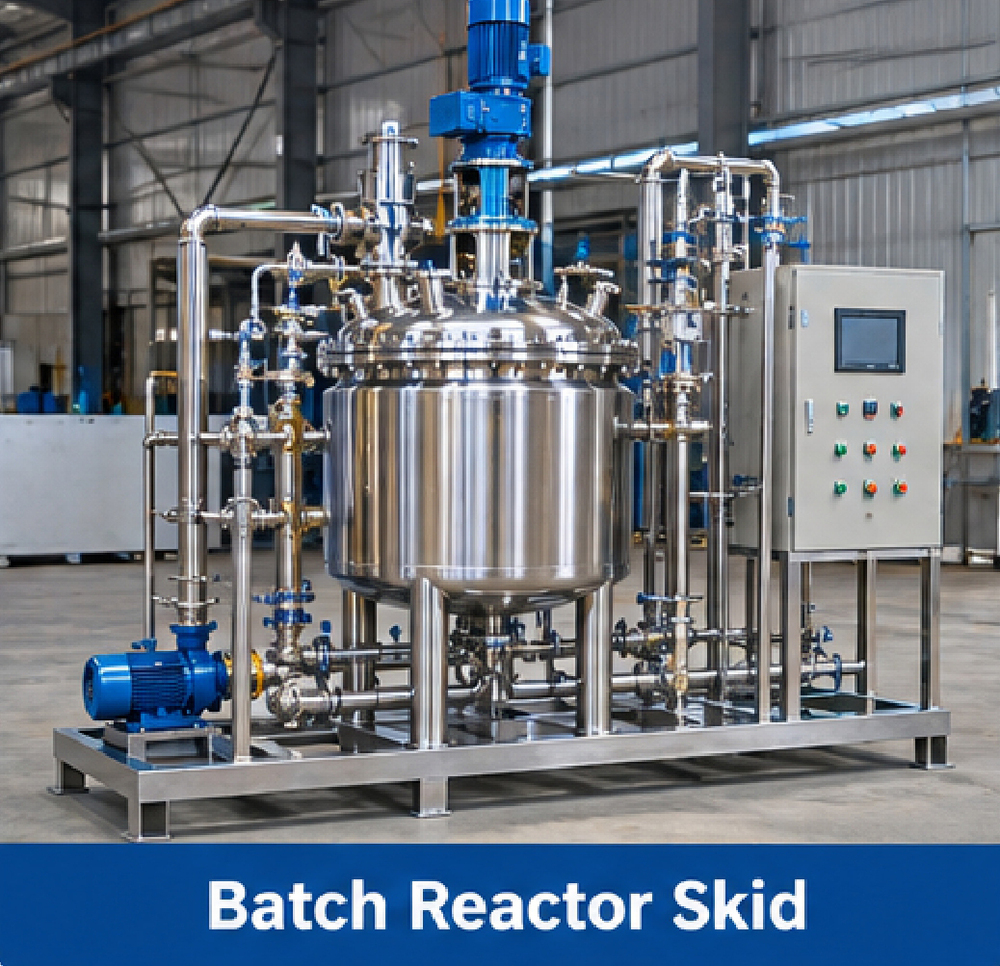
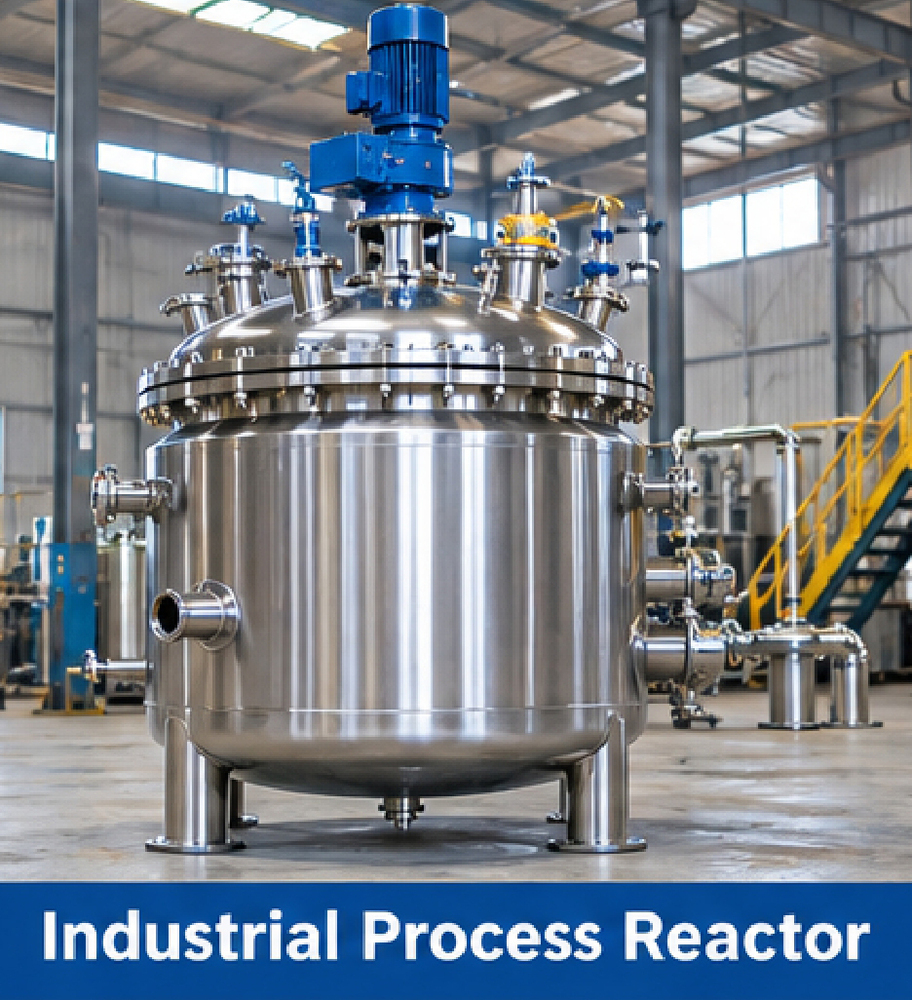
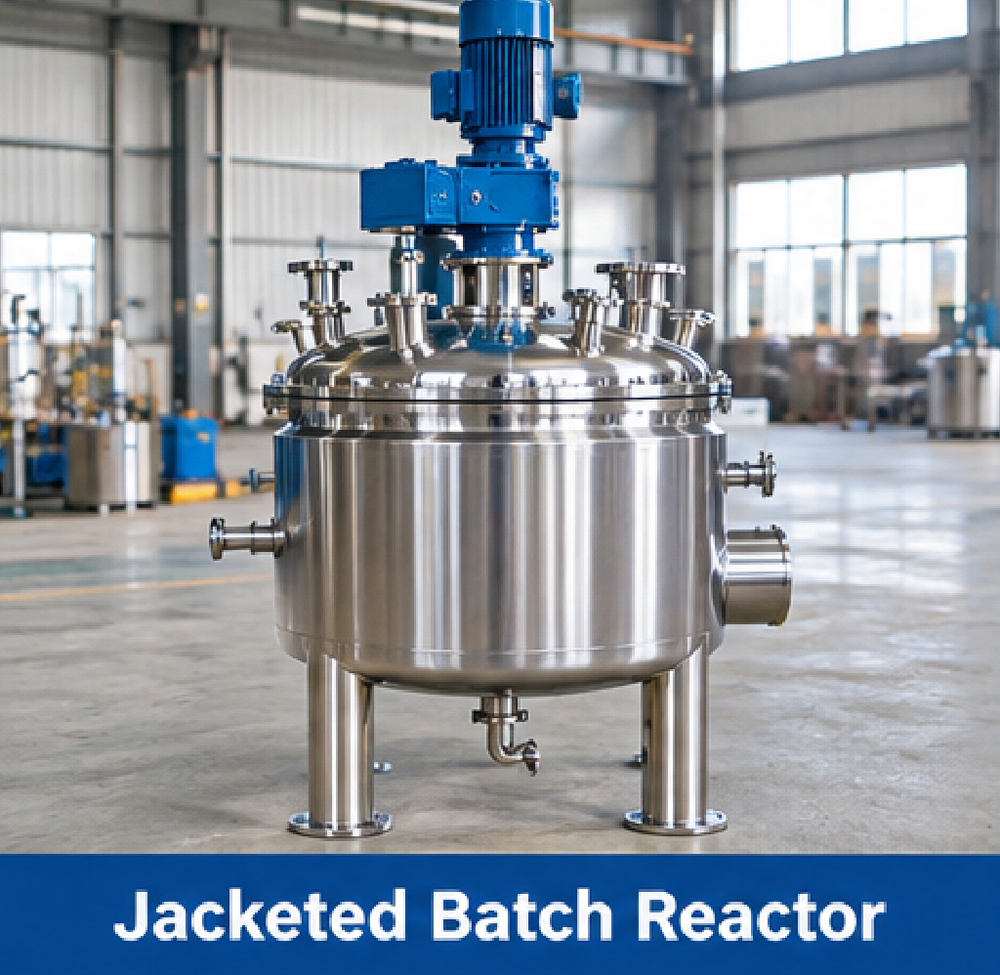
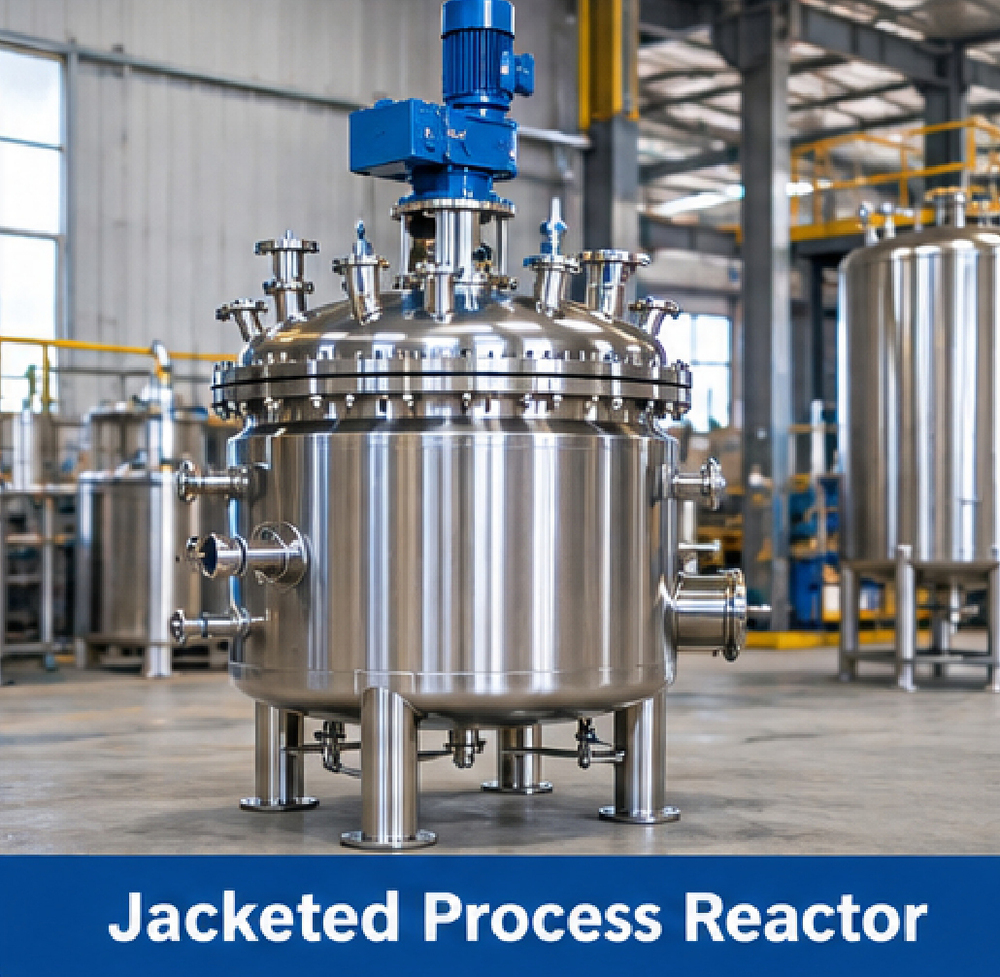
Unlock top-tier efficiency and reliability with our Skid-Mounted Chemical Reactor, designed for valiant industrial chemical processing. Engineered from premium SS304/SS316 stainless steel, this batch reactor features a customizable mirror-polished internal finish and a matte external surface. The modular skid design ensures quick installation and effortless mobility. Equipped with a weatherproof control panel, touchscreen HMI, advanced safety interlocks, and optional insulation, it guarantees optimal performance and secure operation. Shop now to elevate your production with a decorated, customizable solution you can trust.
Distinctive Features and Competitive Advantages
Our Skid-Mounted Chemical Reactor offers unmatched adaptability with capacities ranging from 500 to 10,000 liters and full customization. Special features include seamless SS316 piping, advanced touchscreen HMI controls, robust safety systems, and modular design for rapid installation. Its mirror-polished internal finish and optimized heat insulation boost process hygiene and energy efficiency. These reactors are suited for diverse chemical processing, mixing, and reaction applications in pharmaceutical, chemical, and allied industries, delivering reliability and operational excellence.
Domestic Market Reach and Premium Supply Services
Serving the entire Indian domestic market, we provide premium quality reactors with reliable supply ability and prompt dispatch timelines. Upon receiving your purchase order, our logistics team ensures smooth delivery and installation support. Flexible payment terms cater to varied procurement needs, making it easier for clients to acquire superior technology quickly. With consistent stock availability, robust manufacturing capabilities, and excellent after-sales service, we ensure your investment is protected and rewarded.
FAQ's of Skid-Mounted Chemical Reactor:
Q: How does the skid-mounted design of the chemical reactor benefit installation?
A: The skid-mounted modular design enables quick installation and easy relocation, reducing site disruption and minimizing downtime. Plug-and-play utility connections further simplify setup.
Q: What customizable options are available for the reactor?
A: You can customize the reactor's capacity, dimensions, surface finish, heating system, motor rating, voltage, and various instrumentation to match your operational requirements.
Q: Where can these chemical reactors be used?
A: Designed for versatile application, these reactors are ideal for industrial chemical processing, pharmaceutical manufacturing, mixing, and material reactions in both small and large-scale operations.
Q: What safety features are included in the reactor system?
A: Advanced safety systems include an overpressure relief valve, emergency stop, interlocking controls, and mechanical seals to prevent leaks-all monitored via a user-friendly touchscreen HMI.
Q: How is the product dispatched after a purchase order is placed?
A: Once your purchase order is confirmed, the reactor is promptly dispatched using safe transportation methods suitable for heavy-duty equipment, ensuring it reaches your site efficiently and securely.
Q: What are the main benefits of the computerized, automated, PLC-controlled operation?
A: The fully automated, PLC-controlled system provides consistent process management, real-time monitoring, and precise adjustments, enhancing operational safety, efficiency, and productivity.
 Send Inquiry




 Send Inquiry


 Send Inquiry
